Tube Adapters Buyers’ Guide
Tube adapters are the interface between rod ends and tubing: weld-in chromoly bungs that turn plain tube into a threaded, adjustable, serviceable link. This guide explains why welding a rod end directly never works, the adapter styles, and how to choose across SYZ’s 73 configurations.
What Are Tube Adapters & Weld Bungs?
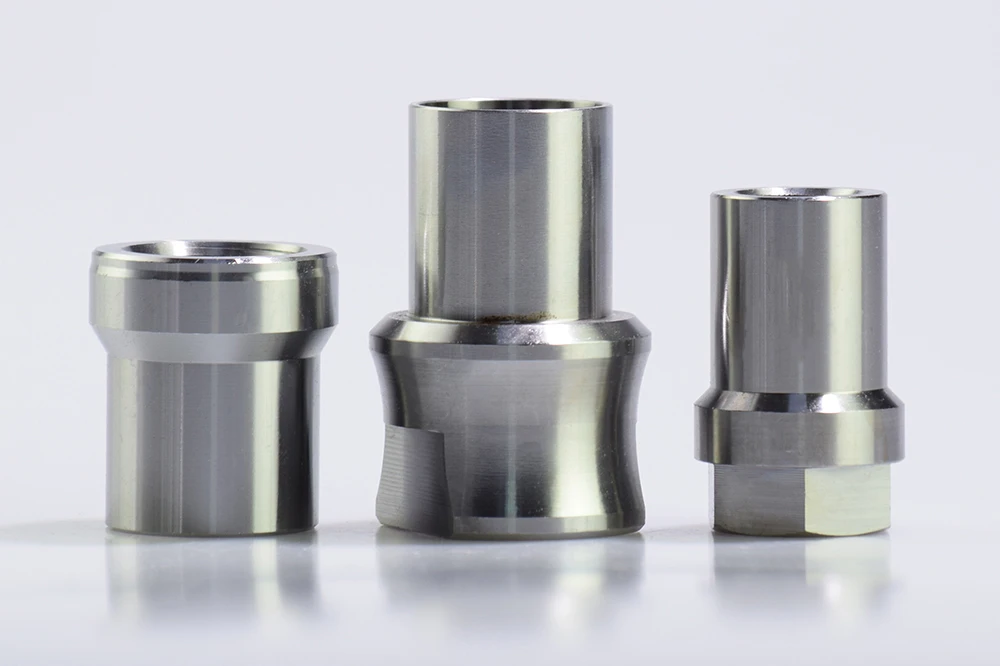
DefinitionTube adapters connect a rod end to tubing. Plain tube has no thread; a rod end has nothing to weld to safely. The adapter bridges that gap: weld the adapter into the tube, let it cool, then thread the rod end in — and the tube becomes an adjustable, serviceable link.
SYZ machines adapters in four families: weld-in tube adapters (the core product), bung adjuster nuts, linkage adjusters and weld-on wrench hexes. Standard material is 4130 chromoly, left-hand parts marked with grooves; inch and metric, with aluminum and titanium custom.
- Also called
- Weld bungs · tube inserts · threaded bungs
- Core function
- Threaded interface between tube and rod end
- Profiles
- Round · hex · square · round-hex
- Thread hands
- RH standard · LH groove-marked
Anatomy of a Weld-In Adapter
StructureThree functional elements — each one a reason the adapter exists.
Weld Shell
The smooth OD sized to your tube’s ID — this is the surface that fuses to the tube. Wall thickness range .058″–.250″ across the 3/8″–2″ tube sizes.
Threaded Bore
The UNF internal thread that receives the rod end — one RH, one LH per link gives turnbuckle adjustment. Threads are protected until assembly.
Profile & Marking
Round for standard arms, hex and square for wrench grip, round-hex hybrids — and left-hand parts groove-marked so they can’t be mixed up on the bench.
Weld-In Adapters (WTF)
Chromoly inserts welded into the tube end, threaded for the rod end: 73 configurations and 146 part numbers covering 3/8″ to 2″ tube ODs in round, hex, square and round-hex profiles.
The standard for suspension arms, steering links and any adjustable fabricated assembly.
Adjuster Hardware
Bung adjuster nuts (RH/LH threaded sleeves), linkage adjusters (female-male bodies) and weld-on wrench hexes complete the adjustable-link system.
Choose these when the link needs in-place length adjustment rather than a fixed thread.
What a Tube Adapter Does in a Link
FunctionFour engineering jobs — starting with the one that protects the rod end.
Protect the rod end from weld heat
Welding a rod end directly destroys the bearing’s heat treatment and melts any PTFE liner — the joint seizes and loses its load rating. The adapter takes the weld instead; the rod end threads in afterward.
Convert tube to thread
Plain tube becomes a threaded, serviceable member: the rod end screws in, adjusts, and can be replaced without cutting.
Enable turnbuckle adjustment
One RH and one LH adapter per link let the tube act as the adjuster — length set in place, locked with jam nuts.
Match the tube package
Adapter OD pairs with tube ID across wall ranges; profile choices (hex/square) add wrench surfaces where the build needs them.
Where adapter selections go wrong
- Welding the rod end in directly — destroyed bearings, no exceptions.
- Mixing up LH and RH adapters — left-hand is groove-marked for a reason.
- Adapter OD mismatched to tube ID — poor weld penetration.
- Forgetting thread protection during welding — spatter in the bore.
Choose the Material
Materials4130 chromoly is the standard; special materials are machined to order.
4130 Chromoly
StandardThe standard material: welds to chromoly/DOM tube with matched strength and takes the weld heat in the shell, not the thread.
Mild Steel
Economy optionAvailable where the structure is mild steel and cost matters — same thread logic.
Aluminum / Titanium
Custom to orderMachined to order for weight-critical racing programs and specialty builds.
Materials and Finishes
Surface treatmentAdapter finishes are set at fabrication — the weld is the finish event.
| Treatment | Applied to | Series examples | What it does |
|---|---|---|---|
| Bare 4130 | Supplied condition | All configs | Clean machined surface ready to weld. |
| Post-weld finishing | Fabrication level | Completed links | Paint or coat after welding; protect threads during the process. |
| Black anodizing | Aluminum customs | Aluminum specials | Finish on aluminum custom adapters. |
Thread, tube-OD and profile charts for all 146 part numbers are on the tube adapters spec page.
Where Tube Adapters Perform
ApplicationsAnywhere a threaded rod end meets a welded tube structure.
Suspension Links
Control arms, radius rods and 4-link bars — one RH + one LH adapter per link.
WTF seriesSteering Systems
Custom tie rods and drag links with turnbuckle adjustment.
WTF seriesAdjustable Links
Combined with bung adjuster nuts and linkage adjusters for fine tuning.
BANLBACustom Fabrication
Special profiles and materials for production programs.
CustomHow to Choose: 5 Steps, Then the Config Table
Selection referenceMatch the Tube
Start from tube OD and wall — the adapter shell must pair with the tube ID for a full-penetration weld.
Match the Rod End Thread
Adapter thread must match the rod end’s shank thread — confirm male/female and size.
Set the Thread Hands
One RH + one LH per link for turnbuckle adjustment; LH parts are groove-marked.
Pick the Profile
Round for clean arms; hex/square where the build needs wrench or anti-rotation faces.
Confirm the Material
4130 chromoly standard; mild steel for economy; aluminum/titanium to order.
| Family | Function | Range | Where |
|---|---|---|---|
| Tube-end thread system | |||
| WTF weld-in adapters | Threaded interface tube ↔ rod end | 73 configs / 146 PN · 3/8″–2″ OD | View |
| Bung adjuster nuts | Internal/external thread adjuster | 15 sizes RH/LH | View |
| Linkage adjusters | Female-male adjuster bodies | 14 sizes · 3 materials | View |
| Weld-on wrench hexes | Wrench flats on tube OD | 13 sizes | View |
Completing the assembly? Pair adapters with chromoly tubing, rod ends and jam nuts — or order a complete linkage rod.
Get Selection HelpTube Adapter Buyers’ Questions
FAQQ1Why can’t I weld the rod end directly to the tube?
Q2How do I tell left-hand adapters apart?
Q3What profiles are available?
Q4What tube sizes do adapters cover?
Q5Are non-chromoly adapters available?
Selecting Tube Adapters?
Send us your tube OD, wall and rod-end threads — SYZ engineers reply with the right adapters and factory-direct pricing from sample to production.