
Round
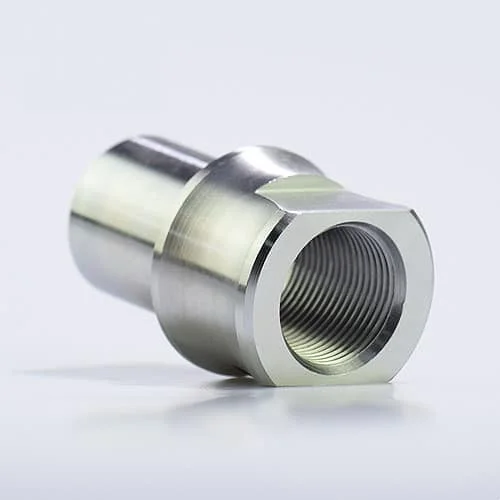
The standard weld-in adapter. Stepped body slips into the tube ID and self-centres for a clean, concentric weld. Use a weld-on wrench hex if you need a grip point.
Search by part number, series, material, application, or specification.
Press Enter to view all results Esc to close
The Interface Between Rod Ends and Tubing
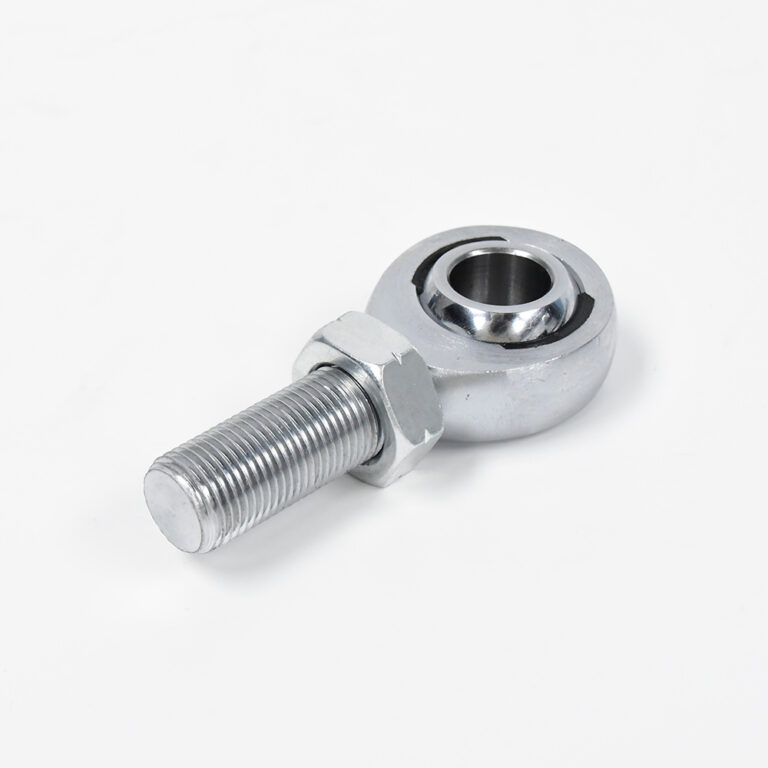
A rod end cannot be welded straight to a tube — welding heat ruins the bearing’s heat treatment and melts the PTFE liner. Tube adapters solve that: weld the adapter into the tube, let it cool, then thread the rod end in. SYZ machines 4130 chromoly weld-in adapters in round, hex, square, round-hex and custom profiles, inch and metric, RH and LH — plus bung adjuster nuts, linkage adjusters and weld-on wrench hexes to finish the link.
Overview
They are the parts that connect a rod end to tubing. Plain tube has no thread; a rod end has nothing to weld to safely. The adapter bridges that gap — and once it is in, the tube becomes an adjustable, serviceable link.
SYZ supplies four families for this job. Tube adapters (weld-in) — chromoly inserts welded into the tube end, with the rod end threading into the adapter. Bung adjuster nuts — a threaded adjuster sleeve, RH one end and LH the other, working like a turnbuckle for length adjustment. Linkage adjusters — a female-male adjuster in carbon steel, chromoly or aluminum. Weld-on wrench hexes — mild-steel hex rings welded onto the tube OD to give a wrench something to grip.
Standard material is 4130 chromoly steel, left hand marked with grooves. Both inch and metric sizes are available, and we machine special sizes and materials to order — including aluminum and titanium.
Body Profiles
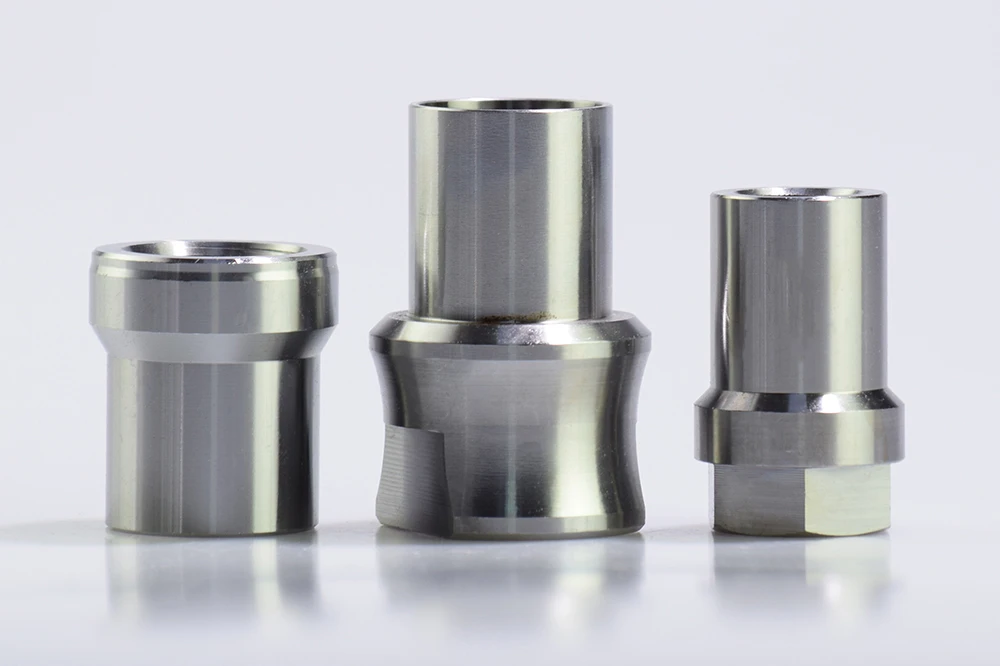
The threaded bore is the same job in every case — the outside profile is what decides how you hold the part and how it sits in the tube.


Product Offerings
| Product | Material | Thread / Sizing | Notable |
|---|---|---|---|
| Tube Adapters WTF series | 4130 chromoly (mild steel optional) | RH & LH female thread 10-32 → 1 1/4-12; tube OD 3/8″ → 2″, wall .058″ → .250″ | 73 configurations (146 part numbers with both hands); LH marked with grooves; hex available |
| Bung Adjuster Nut BAN / BANL series | Chromoly steel, silver zinc plated | Internal thread 3/8-24 → 1 1/4-12; external thread 1/2-20 → 1 1/2-12; hex E 0.563″ → 1.875″ | 15 part numbers; matched RH and LH pairs plus mixed RH/LH variants for turnbuckle action |
| Linkage Adjuster LBA / LBAX / ALBA | LBA carbon steel zinc / LBAX chromoly heat treated / ALBA aluminum black anodized | Thread 3/8-24 → 1 1/4-12, plus M10×1.50 metric; male UNF-3A left hand, female UNF-2B right hand | 14 sizes in each of 3 materials; pick material by load vs weight |
| Weld-On Wrench Hexes 1865 series | Mild steel (weldable) | Fits tubing OD 3/8″ → 2″; wrench size 5/8″ → 2 1/4″ | 13 sizes; adds a wrench flat to round tube |
| Part No. (RH) | Part No. (LH) | Tube Size (OD × Wall) | Female Thread |
|---|---|---|---|
| WTF-0301R | WTF-0301L | 3/8″ OD x 0.058 | 10-32 |
| WTF-0401R | WTF-0401L | 1/2″ OD x 0.058 | 1/4-28 |
| WTF-0501R | WTF-0501L | 1/2″ OD x 0.058 | 5/16-24 |
| WTF-0502R | WTF-0502L | 5/8″ OD x 0.058 | 5/16-24 |
| WTF-0601R | WTF-0601L | 5/8″ OD x 0.058 | 3/8-24 |
| WTF-0701R | WTF-0701L | 5/8″ OD x 0.058 | 7/16-20 |
| WTF-0402R | WTF-0402L | 3/4″ OD x 0.058 | 1/4-28 |
| WTF-0503R | WTF-0503L | 3/4″ OD x 0.058 | 5/16-24 |
| WTF-0602R | WTF-0602L | 3/4″ OD x 0.058 | 3/8-24 |
| WTF-0702R | WTF-0702L | 3/4″ OD x 0.058 | 7/16-20 |
| WTF-0504R | WTF-0504L | 3/4″ OD x 0.065 | 5/16-24 |
| WTF-0603R | WTF-0603L | 3/4″ OD x 0.065 | 3/8-24 |
| WTF-0703R | WTF-0703L | 3/4″ OD x 0.065 | 7/16-20 |
| WTF-0604R | WTF-0604L | 7/8″ OD x 0.058 | 3/8-24 |
| WTF-0704R | WTF-0704L | 7/8″ OD x 0.058 | 7/16-20 |
| WTF-0801R | WTF-0801L | 7/8″ OD x 0.058 | 1/2-20 |
| WTF-0605R | WTF-0605L | 7/8″ OD x 0.065 | 3/8-24 |
| WTF-0705R | WTF-0705L | 7/8″ OD x 0.065 | 7/16-20 |
| WTF-0802R | WTF-0802L | 7/8″ OD x 0.065 | 1/2-20 |
| WTF-0606R | WTF-0606L | 7/8″ OD x 0.083 | 3/8-24 |
| WTF-0706R | WTF-0706L | 7/8″ OD x 0.083 | 7/16-20 |
| WTF-0803R | WTF-0803L | 7/8″ OD x 0.083 | 1/2-20 |
| WTF-0607R | WTF-0607L | 1″ OD x 0.058 | 3/8-24 |
| WTF-0707R | WTF-0707L | 1″ OD x 0.058 | 7/16-20 |
| WTF-0804R | WTF-0804L | 1″ OD x 0.058 | 1/2-20 |
| WTF-1001R | WTF-1001L | 1″ OD x 0.058 | 5/8-18 |
| WTF-0608R | WTF-0608L | 1″ OD x 0.065 | 3/8-24 |
| WTF-0708R | WTF-0708L | 1″ OD x 0.065 | 7/16-20 |
| WTF-0805R | WTF-0805L | 1″ OD x 0.065 | 1/2-20 |
| WTF-1002R | WTF-1002L | 1″ OD x 0.065 | 5/8-18 |
| WTF-0609R | WTF-0609L | 1″ OD x 0.083 | 3/8-24 |
| WTF-0709R | WTF-0709L | 1″ OD x 0.083 | 7/16-20 |
| WTF-0806R | WTF-0806L | 1″ OD x 0.083 | 1/2-20 |
| WTF-1003R | WTF-1003L | 1″ OD x 0.083 | 5/8-18 |
| WTF-0610R | WTF-0610L | 1″ OD x 0.095 | 3/8-24 |
| WTF-0710R | WTF-0710L | 1″ OD x 0.095 | 7/16-20 |
| WTF-0807R | WTF-0807L | 1″ OD x 0.095 | 1/2-20 |
| WTF-1004R | WTF-1004L | 1″ OD x 0.095 | 5/8-18 |
| WTF-0808R | WTF-0808L | 1 1/8″ OD x 0.058 | 1/2-20 |
| WTF-1005R | WTF-1005L | 1 1/8″ OD x 0.058 | 5/8-18 |
| WTF-0809R | WTF-0809L | 1 1/8″ OD x 0.065 | 1/2-20 |
| WTF-1006R | WTF-1006L | 1 1/8″ OD x 0.065 | 5/8-18 |
| WTF-0810R | WTF-0810L | 1 1/8″ OD x 0.083 | 1/2-20 |
| WTF-1007R | WTF-1007L | 1 1/8″ OD x 0.083 | 5/8-18 |
| WTF-1201R | WTF-1201L | 1 1/8″ OD x 0.083 | 3/4-16 |
| WTF-0811R | WTF-0811L | 1 1/8″ OD x 0.095 | 1/2-20 |
| WTF-1008R | WTF-1008L | 1 1/8″ OD x 0.095 | 5/8-18 |
| WTF-1202R | WTF-1202L | 1 1/8″ OD x 0.095 | 3/4-16 |
| WTF-1009R | WTF-1009L | 1 1/4″ OD x 0.095 | 5/8-18 |
| WTF-1203R | WTF-1203L | 1 1/4″ OD x 0.095 | 3/4-16 |
| WTF-1010R | WTF-1010L | 1 1/4″ OD x 0.120 | 5/8-18 |
| WTF-1204R | WTF-1204L | 1 1/4″ OD x 0.120 | 3/4-16 |
| WTF-1011R | WTF-1011L | 1 3/8″ OD x 0.095 | 5/8-18 |
| WTF-1205R | WTF-1205L | 1 3/8″ OD x 0.095 | 3/4-16 |
| WTF-1012R | WTF-1012L | 1 3/8″ OD x 0.120 | 5/8-18 |
| WTF-1206R | WTF-1206L | 1 3/8″ OD x 0.120 | 3/4-16 |
| WTF-1013R | WTF-1013L | 1 1/2″ OD x 0.095 | 5/8-18 |
| WTF-1207R | WTF-1207L | 1 1/2″ OD x 0.095 | 3/4-16 |
| WTF-1208R | WTF-1208L | 1 1/2″ OD x 0.120 | 3/4-16 |
| WTF-1401R | WTF-1401L | 1 1/2″ OD x 0.120 | 7/8-14 |
| WTF-1209R | WTF-1209L | 1 1/2″ OD x 0.250 | 3/4-16 |
| WTF-1402R | WTF-1402L | 1 1/2″ OD x 0.250 | 7/8-14 |
| WTF-1210R | WTF-1210L | 1 3/4″ OD x 0.120 | 3/4-16 |
| WTF-1403R | WTF-1403L | 1 3/4″ OD x 0.120 | 7/8-14 |
| WTF-1601R | WTF-1601L | 1 3/4″ OD x 0.120 | 1-14 |
| WTF-2001R | WTF-2001L | 1 3/4″ OD x 0.120 | 1 1/4-12 |
| WTF-1211R | WTF-1211L | 1 3/4″ OD x 0.250 | 3/4-16 |
| WTF-1404R | WTF-1404L | 1 3/4″ OD x 0.250 | 7/8-14 |
| WTF-1602R | WTF-1602L | 1 3/4″ OD x 0.250 | 1-14 |
| WTF-2002R | WTF-2002L | 2″ OD x 0.250 | 1 1/4-12 |
| WTF-1603R | WTF-1603L | 2″ OD x 0.250 | 1-14 |
| WTF-1604R | WTF-1604L | 2″ OD x 0.250 | 1-12 |
| WTF-2003R | WTF-2003L | 2″ OD x 0.120 | 1 1/4-12 |
Material: 4130 chromoly steel (mild steel optional). Left hand parts are marked with grooves. Hex available; special sizes available in volume — send a print or a sample. Filter and quote by part number on the tube adapter spec page.
| Part No. | Internal Thread C | External Thread D | Hex E | Length A | Hex Len. B |
|---|---|---|---|---|---|
| BAN-8-6 | 3/8-24 RH | 1/2-20 RH | 0.563 | 1.250 | 0.219 |
| BANL-8-6 | 3/8-24 LH | 1/2-20 LH | 0.563 | 1.250 | 0.219 |
| BAN-10-8 | 1/2-20 RH | 5/8-18 RH | 0.750 | 1.500 | 0.313 |
| BANL-10-8 | 1/2-20 LH | 5/8-18 LH | 0.750 | 1.500 | 0.313 |
| BAN-12-10 | 5/8-18 RH | 3/4-16 RH | 0.938 | 1.630 | 0.375 |
| BANL-12-10 | 5/8-18 LH | 3/4-16 LH | 0.938 | 1.630 | 0.375 |
| BAN-12-10-1 | 5/8-18 RH | 3/4-16 LH | 0.938 | 1.630 | 0.375 |
| BAN-16-12 | 3/4-16 RH | 1-12 RH | 1.125 | 1.750 | 0.422 |
| BANL-16-12 | 3/4-16 LH | 1-12 LH | 1.125 | 1.750 | 0.422 |
| BAN-16-12-1 | 3/4-16 LH | 1-12 RH | 1.125 | 1.750 | 0.422 |
| BANL-16-12-1B | 3/4-16 LH | 1-12 RH | 1.125 | 2.750 | 0.422 |
| BAN-20-16 | 1 – 12 RH | 1 1/4-12 RH | 1.500 | 2.130 | 0.547 |
| BANL-20-16 | 1 – 12 LH | 1 1/4-12 LH | 1.500 | 2.130 | 0.547 |
| BAN-24-20 | 1 1/4-12 RH | 1 1/2-12 RH | 1.875 | 2.130 | 0.719 |
| BANL-24-20 | 1 1/4-12 LH | 1 1/2-12 LH | 1.875 | 2.130 | 0.719 |
Chromoly steel, silver zinc plated, allows adjustment with a thread bung. Note the mixed-hand parts — BAN-12-10-1, BAN-16-12-1 and BANL-16-12-1B combine RH and LH in one body, which is what gives you turnbuckle action from a single nut. Special sizes available in volume.
| Part No. | Fits Tubing OD | Wrench Size | I.D. Size |
|---|---|---|---|
| 1865-101 | 3/8″ | 5/8″ | 0.390 |
| 1865-102 | 1/2″ | 3/4″ | 0.515 |
| 1865-103 | 5/8″ | 7/8″ | 0.640 |
| 1865-104 | 3/4″ | 1″ | 0.765 |
| 1865-105 | 7/8″ | 1 1/8″ | 0.890 |
| 1865-106 | 1″ | 1 1/4″ | 1.015 |
| 1865-107 | 1 1/8″ | 1 3/8″ | 1.140 |
| 1865-108 | 1 1/4″ | 1 1/2″ | 1.265 |
| 1865-109 | 1 3/8″ | 1 5/8″ | 1.390 |
| 1865-110 | 1 1/2″ | 1 3/4″ | 1.515 |
| 1865-111 | 1 5/8″ | 1 7/8″ | 1.640 |
| 1865-112 | 1 3/4″ | 2″ | 1.765 |
| 1865-113 | 2″ | 2 1/4″ | 2.015 |
Mild steel, fits different tube OD sizes. Slide it over the tube, weld it on, and you have a flat to hold while setting link length. The I.D. column is the bore — match it to your tube OD.
| Carbon Steel | Chromoly Steel | Aluminum | Thread (M & F) | Length A Ref. |
|---|---|---|---|---|
| LBA6-19 | LBAX6-19 | ALBA6-19 | 3/8-24 | 1.850 |
| LBA6-29 | LBAX6-29 | ALBA6-29 | 3/8-24 | 2.875 |
| LBA6-34 | LBAX6-34 | ALBA6-34 | 3/8-24 | 3.435 |
| LBA7-31 | LBAX7-31 | ALBA7-31 | 7/16-20 | 3.125 |
| LBA8-34 | LBAX8-34 | ALBA8-34 | 1/2-20 | 3.375 |
| LBA8-36 | LBAX8-36 | ALBA8-36 | 1/2-20 | 3.625 |
| LBA10-38 | LBAX10-38 | ALBA10-38 | 5/8-18 | 3.813 |
| LBA10-39 | LBAX10-39 | ALBA10-39 | 5/8-18 | 3.875 |
| LBA12-41 | LBAX12-41 | ALBA12-41 | 3/4-16 | 4.125 |
| LBA12-41-1 | LBAX12-41-1 | ALBA12-41-1 | 3/4-16 | 4.125 |
| LBA12-47 | LBAX12-47 | ALBA12-47 | 3/4-16 | 4.650 |
| LBA16-61 | LBAX16-61 | ALBA16-61 | 1 – 12 | 6.125 |
| LBA20-66 | LBAX20-66 | ALBA20-66 | 1.25-12 | 6.625 |
| LBA-M10 | LBAX-M10 | ALBA-M10 | M10 x 1.50 | 88mm |
Female-male adjuster. Male thread is UNF-3A left hand, female thread is UNF-2B right hand — so the adjuster is inherently a turnbuckle. LBA is carbon steel silver zinc plated; LBAX is heat-treated chromoly, silver zinc plated; ALBA is aluminum, black anodized — the weight-saving option and the one to use with aluminum rod ends. Full B/C/D/E dimensions on the linkage adjuster spec page.
Engineering Guide
Four decisions, in this order. Get them right and the chart above gives you a part number.
Fabrication Guide
Non-negotiable. Weld heat destroys the bearing and the PTFE liner. Back it out before you strike an arc.
Mill scale, cutting oil and drawing lube all cause porosity. Clean both mating surfaces before assembly.
Thread a sacrificial bolt or an old rod end into the adapter while you weld. It acts as a heat sink and keeps the thread from distorting — cheaper than chasing it afterwards.
Evenly spaced tacks limit distortion and keep the adapter square in the tube.
Then let it cool slowly in still air. Do not quench 4130 — see the chromoly tubing guide for filler rod selection.
Cool completely, then run a tap through if the weld tightened the thread, and check concentricity so the rod end does not bind.
Sizing Example
Say you are building an adjustable 4-link bar around a 3/4-16 male chromoly rod end, using 1-1/2″ OD × 0.120″ wall DOM tube:
Matches the rod end. That is the first filter on the chart.
1.5″ − (2 × 0.120″) = 1.26″. On the chart, 1 1/2″ OD × 0.120 with a 3/4-16 female thread is WTF-1208R and WTF-1208L.
WTF-1208R at one end, WTF-1208L at the other, so the finished bar adjusts like a turnbuckle.
Round tube has no flats, so add a weld-on wrench hex sized to 1-1/2″ tube OD — part 1865-110 — or specify hex-body adapters instead.
Set the length, then lock both ends with a jam nut. Same logic for any link — only the thread and tube numbers change.
Engineering Detail
Use this compact checklist before welding or adjusting a tube adapter assembly.
| Failure Mode | Likely Cause | Prevention |
|---|---|---|
| Thread binds after welding | Heat shrinkage or off-centre welding | Use a sacrificial bolt as a heat sink, tack in three or more spots, cool slowly and tap after cooling. |
| Weld cracks or adapter pulls out | Sloppy fit, incomplete penetration or tacks carrying the load | Match adapter OD to tube ID and complete the circumferential weld with the correct 4130 procedure. |
| Bearing seizes | Rod end installed during welding | Remove the rod end before welding; heat can destroy the bearing and PTFE liner. |
| Adjustment slips or corrodes | No jam nut, insufficient engagement or dissimilar-metal exposure | Lock both ends with jam nuts, retain full thread engagement and use the correct aluminum option for aluminum tubing. |
Industrial Uses
Custom Programs
Anything not on the chart above is a custom job, and custom is routine here. This is how it runs.
FAQ
Our Strengths
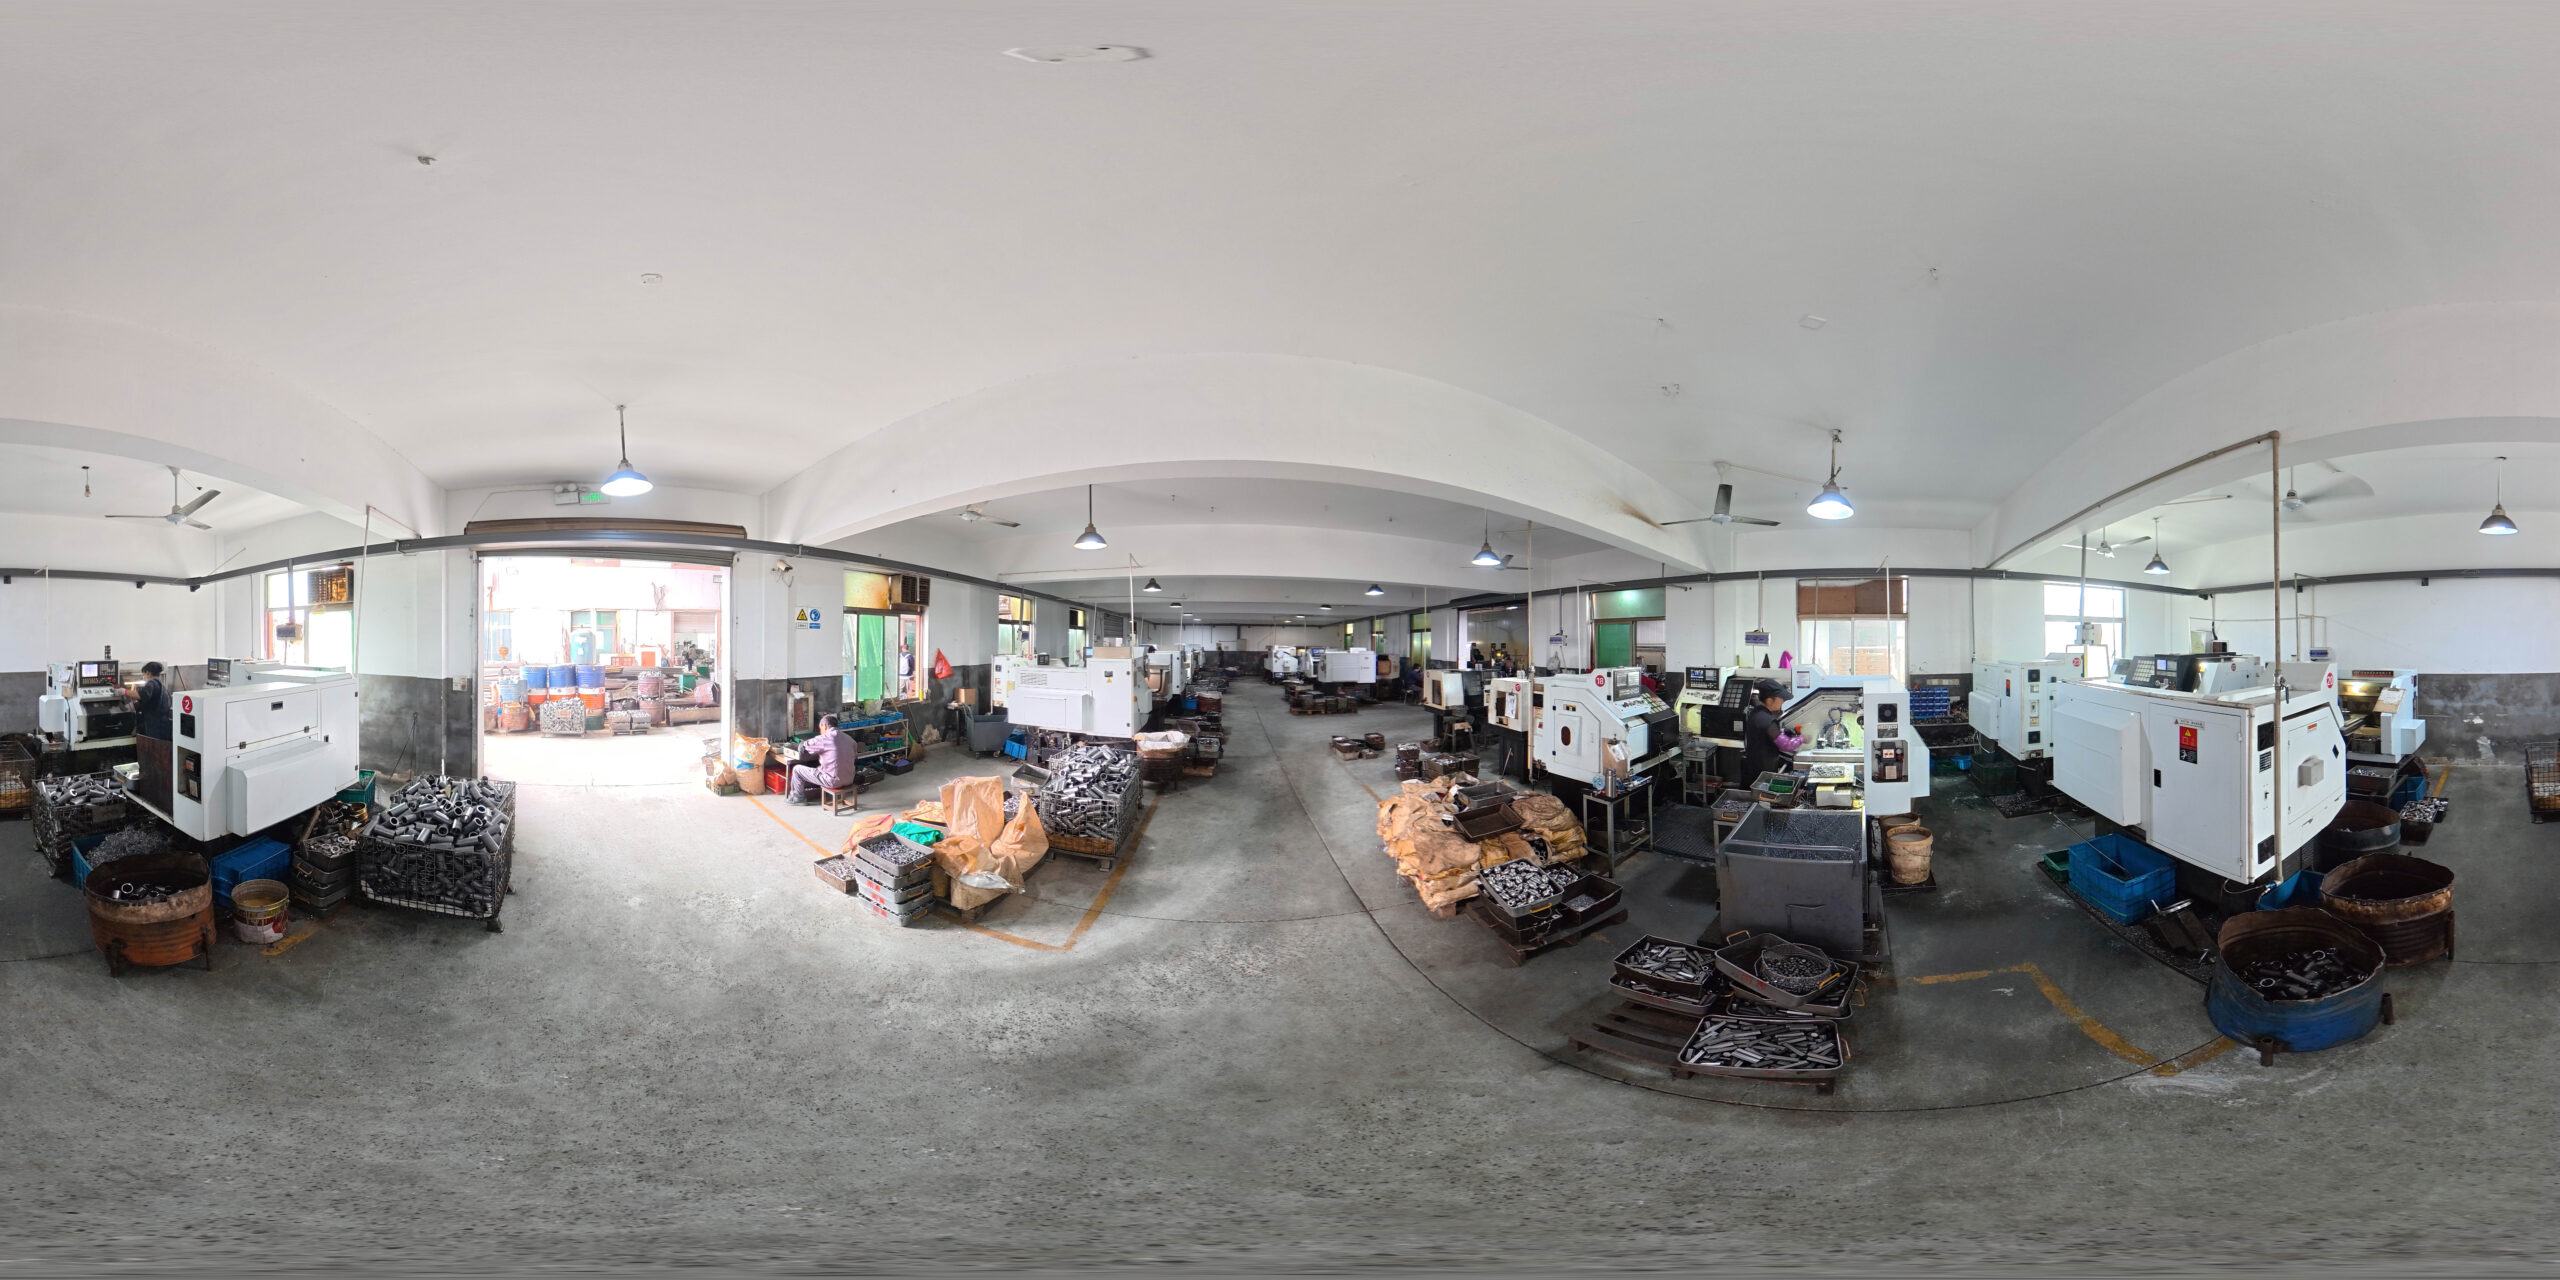
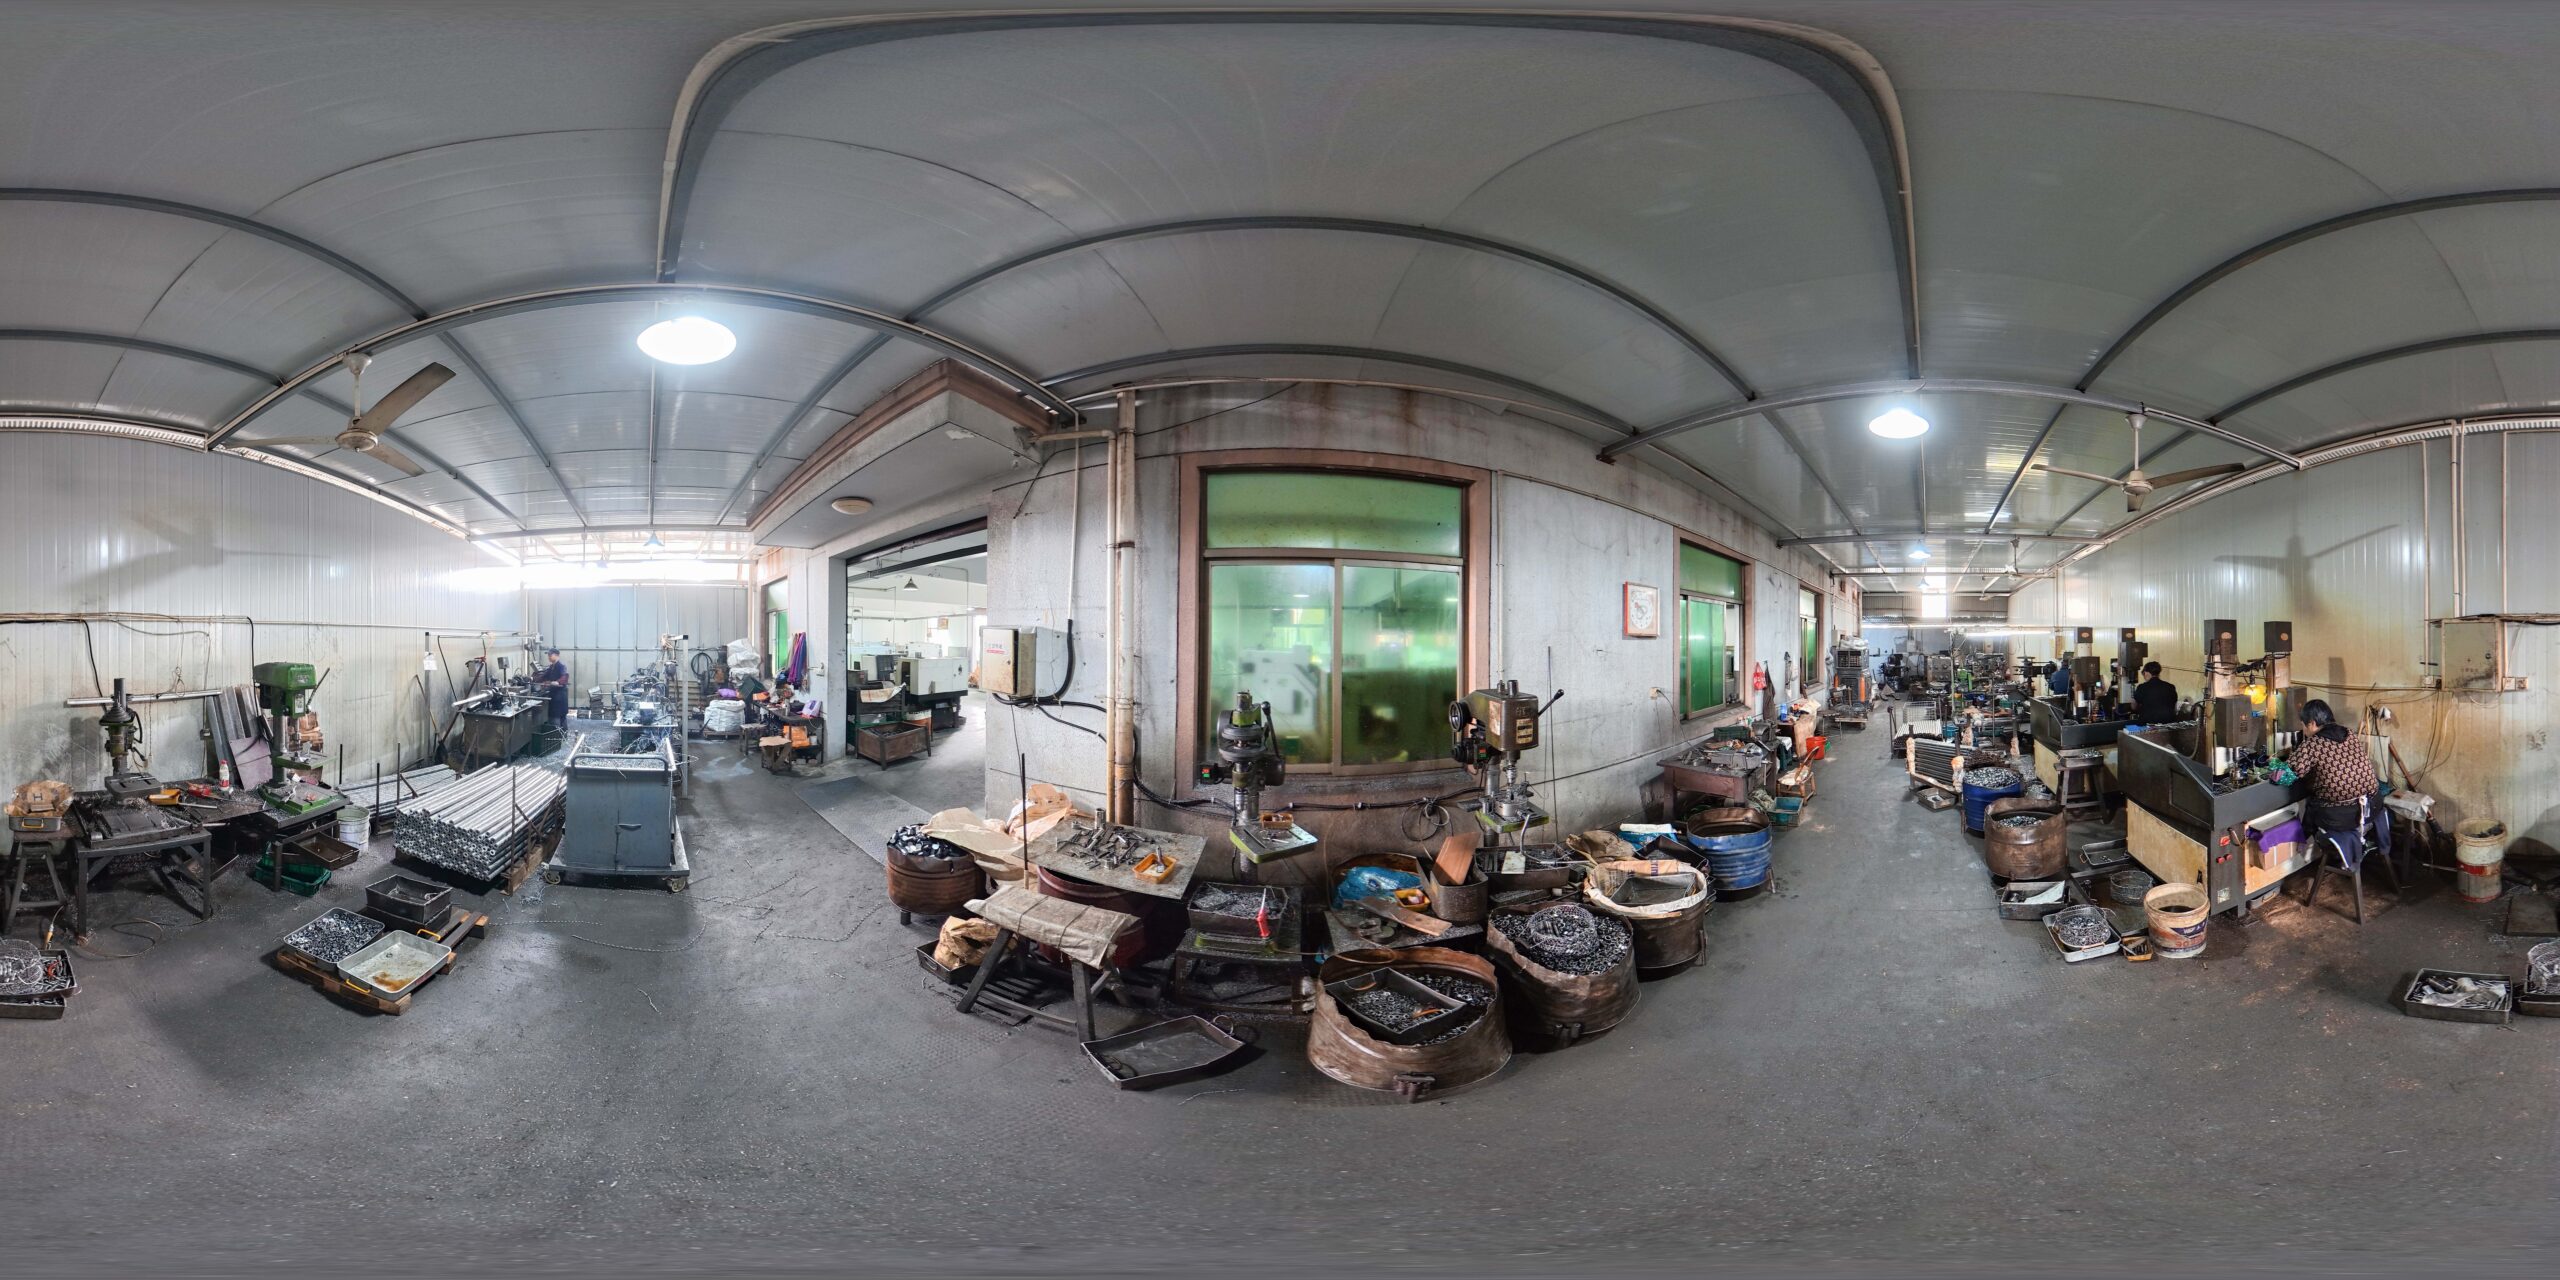
We are a manufacturer of weld-in tube adapter and tube insert solutions, specialising in the design and production of high-quality tube inserts and tube adapters. Years of expertise go into durable, precise, customisable products supplied worldwide to automotive manufacturing, industrial equipment and motorsport fabrication. Continuous innovation and rigorous quality control keep every product to standard — the goal is to be a long-term partner that improves your product performance and your production economics, not a one-off vendor.


Engineering Tools
Buyer Guides
Factory Direct
Leave your request details — part numbers, thread, tube OD and wall, quantities — and we reply within 24 hours with pricing and lead time.